Sanghvi Crane

Top 10 Threaded Inserts for Global Buyers?

Threaded inserts are small components with outsized consequences. A brass insert pressed into a plastic enclosure, or a steel insert seated in plywood, can determine whether a joint survives repeated assembly. For global buyers, the challenge is not simply finding a low unit price. Material, installation method, pull-out resistance, corrosion exposure, and supplier consistency all matter.

Grand View Research valued the broader global fasteners market at approximately USD 90.6 billion in 2023 and forecast 5.5% annual growth from 2024 to 2030. That figure covers many fastener categories, not threaded inserts alone. Still, it signals a large, competitive supply chain where specifications deserve close attention. Richard T. Barrett’s NASA Fastener Design Manual offers a useful engineering principle: select fastening components for the actual loads and service conditions. This is a paraphrase, not a direct quotation. A verified verbatim statement from a threaded-insert specialist was not available, so attributing invented words would undermine buyer confidence.

Details matter. A knurled insert may grip a molded plastic boss well, yet fail if the boss is too thin. A heat-set insert can produce a tidy result, but temperature control and operator skill affect installation. Small differences show up later. This guide compares ten threaded-insert options for international buyers, focusing on application fit, materials, installation, quality evidence, and sourcing questions. It is not a universal ranking: the best choice changes with substrate, load, production volume, and environment. Even a careful shortlist has limits. Verify dimensions, test samples, and confirm the supplier’s documentation before committing to volume orders.
Top 10 Threaded Inserts for Global Buyers?

What Threaded Inserts Are and How They Create Durable Threads

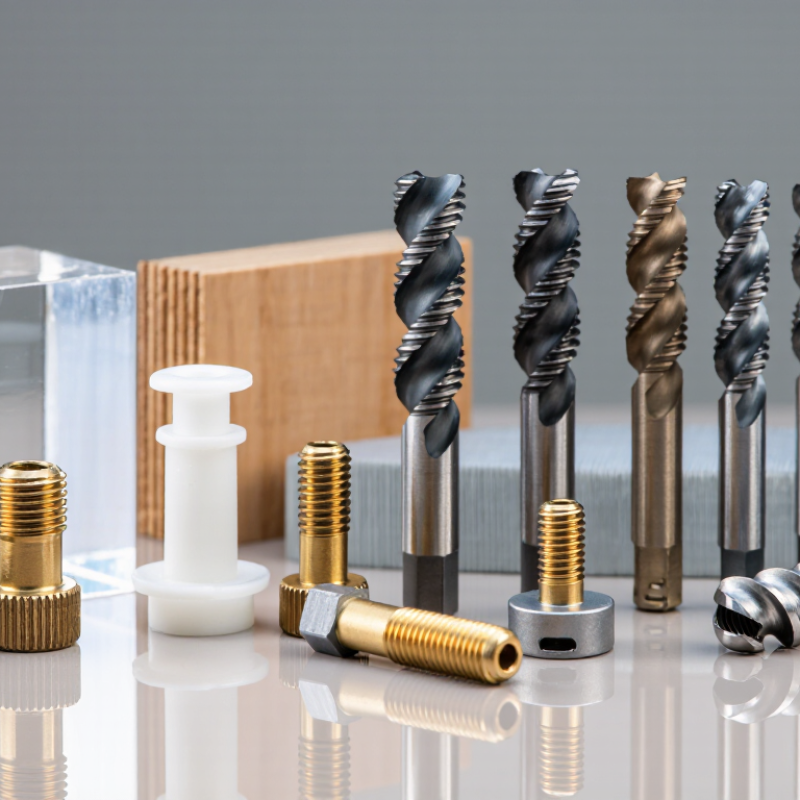
Threaded inserts create durable internal threads by moving screw loads away from materials that wear or strip easily. They are commonly used in plastics, wood, composites, and light metals. Options include press-fit, heat-set, molded-in, and helical inserts; each requires a suitable hole and installation method. For example, a heat-set insert is warmed and pressed into a plastic boss. The softened polymer flows around its knurls, then grips the insert as it cools. The screw engages metal instead of repeatedly cutting plastic. This helps with repeated assembly, but cannot strengthen a weak or thin boss. Selection depends on load, temperature, wall thickness, access, and removal frequency. Details matter.

Tips: Check the specified hole diameter, insertion depth, and installation temperature before production. Test a sample part and inspect for cracks, rotation, and flush seating. Tighten gradually.

Buyers should compare thread size, base material, corrosion resistance, tolerances, and inspection records—not just price. Ask suppliers to identify their test methods; drawings and fit assumptions can differ. A neat-looking insert may still loosen under vibration or repeated removal. Prototype under actual loads and environmental conditions before fixing the design. That step is easy to postpone, and worth reconsidering.

The Main Types of Threaded Inserts and Their Installation Methods

Top 10 Threaded Inserts for Global Buyers?

Threaded inserts create durable threads in materials that cannot hold repeated screw cycles reliably. Common choices include press-fit, self-tapping, heat-set, ultrasonic, molded-in, and helical wire inserts. Each suits different materials and production methods. Press-fit inserts enter a prepared hole through controlled pressure. The hole size matters. Too tight, and the host material may crack; too loose, and the insert can rotate under load. Self-tapping inserts cut or form their own threads in a correctly sized pilot hole, often in metal or plastic.

For thermoplastics, heat-set inserts are pressed into a preformed hole with a heated installation tip. Ultrasonic installation uses vibration to soften surrounding plastic, then allows it to solidify around the insert. Both methods need steady alignment and enough cooling time before loading. Molded-in inserts are positioned in the mold before material is injected, making placement repeatable but increasing setup demands. Helical wire inserts, by contrast, fit into a tapped hole and can restore or reinforce internal threads. Check the insert maker’s specified hole size, material compatibility, installation depth, and torque guidance. Test a sample part. A clean installation can still fail if the surrounding wall is too thin, and that detail is easy to overlook.

Top 10 Threaded Inserts for Global Buyers? - The Main Types of Threaded Inserts and Their Installation Methods

No. Threaded Insert Type Typical Substrate Common Installation Method Typical Uses and Selection Considerations
1 Wire thread insert Metals such as aluminum, magnesium, and steel Drill and tap the hole with the specified insert tap; wind the insert into place with an installation tool, then remove the driving tang when applicable. Creates or repairs an internal thread. Check the required insert length, finished thread size, parent material, and installation-tool requirements.
2 Key-locking solid insert Metal parts, including components subject to repeated assembly Prepare and tap the specified hole, install the solid insert, and drive its locking keys into the parent material using the specified tool. Provides a solid internal thread with mechanical key locking. Confirm the required hole dimensions and available material thickness.
3 Self-tapping insert Metal, plastic, or other materials, depending on insert design Drill a correctly sized pilot hole, then screw the insert into it so its external features cut or form the mating thread. Can avoid a separate tapping operation. Pilot-hole size, material hardness, wall thickness, and installation torque are important.
4 Press-fit insert Plastics and other materials suited to interference-fit installation Align the insert with a prepared hole and press it in using a press or suitable assembly fixture. Knurls, ribs, or other external features can resist rotation or pullout. Match the insert and hole tolerances to the substrate.
5 Heat-set insert Thermoplastics Place the insert in a prepared hole and apply controlled heat and pressure, commonly with a heated installation tip. Used to provide reusable machine-screw threads in plastic parts. Temperature, tip alignment, insertion depth, and cooling time affect the result.
6 Ultrasonic insert Thermoplastics Position the insert in a prepared hole and use an ultrasonic installation tool to soften the surrounding plastic as the insert is pressed into place. Suitable for production assembly when compatible equipment and process control are available. Confirm plastic compatibility and hole geometry.
7 Mold-in insert Plastic parts made by molding Locate the insert in the mold before the plastic is injected; the molded material forms around its external features. Integrates the insert during part manufacture. The mold must hold it securely, and insert position and molding conditions require validation.
8 Blind rivet nut Sheet metal, tubing, and assemblies accessible from one side Place the rivet nut in a prepared hole and use a rivet-nut setting tool to pull its body into a blind-side bulge that clamps the workpiece. Provides an internal thread where rear access is limited. Select the correct grip range, hole size, material, and setting tool.
9 Wood insert with external screw thread Hardwood, softwood, plywood, and some engineered wood products Drill the recommended pilot hole and drive or screw the insert into the workpiece using its installation feature. Creates a reusable machine-thread connection in wood. Pilot-hole size, edge distance, wood type, and installation direction can affect holding strength.
10 Expansion-style threaded insert Selected masonry or other compatible solid materials Drill a hole to the specified size, insert the assembly, and tighten or activate the mechanism to expand it against the hole wall. Used for anchoring threaded connections in compatible base materials. Check the material condition, embedment depth, edge distance, and load requirements.

Installation details and load capacity vary by insert design, dimensions, and substrate. Use the specified hole preparation, tooling, and installation procedure for the selected insert.

Ten Threaded Inserts Compared by Design, Material, and Application

Threaded inserts vary in shape, material, and installation method, so the best choice depends on the part and its service conditions. Heat-set inserts, often made from brass, soften surrounding thermoplastic during installation and suit repeatable assembly. Press-fit inserts use knurls or ribs to grip a prepared hole; they work well in rigid plastics and light-metal components. Ultrasonic inserts are driven into thermoplastics with vibration, but require controlled tooling. Overmolded inserts are placed in a mold before plastic is formed around them. They can provide a stable anchor, though positioning errors are difficult to correct.

Self-tapping inserts cut or form their own threads in a pilot hole, making them useful for some plastics and softer metals. Screw-in inserts have external threads for installation in wood or composite panels. Key-locking inserts add keys that resist rotation, often in metal repairs. Wire-thread inserts use a coiled wire to reinforce tapped holes, especially where threads face repeated service. Fit matters.

Blind or rivet-nut inserts install from one side of a sheet, creating a threaded point where rear access is limited. Wood inserts, commonly threaded externally and internally, anchor fasteners in furniture and panels. Material compatibility, wall thickness, load direction, and installation access should guide selection. A stronger insert is not automatically better. Test samples in the actual substrate; hole size and installation force can change the result. One detail is easy to overlook: removal and repair needs deserve consideration too.

How Global Buyers Match Inserts to Materials and Performance Needs

Global buyers should select threaded inserts by substrate, installation method, and expected load—not by thread size alone. Grand View Research’s Fasteners Market report estimated the global market at US$90.65 billion in 2023, reflecting the scale and variety of fastening needs. That breadth makes a universal insert unlikely. Small details matter.

For plastics, heat-set and ultrasonic inserts can provide durable threads, but wall thickness and resin type affect pull-out strength. For wood or soft composites, coarse external knurls or wide flanges can improve grip.

Metal parts may call for press-fit, keyed, or wire-thread inserts, depending on vibration, repair needs, and available material around the hole. ASM Handbook, Volume 2, lists typical thermal expansion near 23 µm/m·°C for aluminum and about 12 for carbon steel. That difference can affect fit across temperature changes.

Buyers should check substrate data and test installation torque, pull-out force, and vibration performance. A catalog table cannot settle every case. I would also question any selection based only on nominal load; real assemblies vary, sometimes annoyingly, with hole quality and installer technique.

How to Assess Supplier Quality, Standards, and Total Landed Cost

Buying threaded inserts across borders is not just a unit-price exercise. A low quote may exclude sorting, special packaging, or replacement costs after a batch fails inspection. Ask suppliers for controlled drawings, material and coating records, and lot-level traceability. For critical assemblies, request sample results from thread-gauge checks and pull-out tests. Match each test method to the insert, substrate, and expected load. Do not assume one certificate covers every production lot.

Standards vary. Confirm which dimensional, material, and performance requirements apply to your design, then compare them in writing. Check how the supplier controls tool wear, coating thickness, and inspection frequency; these details often reveal more than polished brochures. If corrosion matters, specify exposure conditions rather than requesting “good corrosion resistance.” That wording is vague. Even a careful checklist can miss a mismatch between a drawing revision and the purchase order.

Calculate total landed cost using unit price, tooling, freight, insurance, duties, brokerage, inspection, and expected scrap. Compare quotes on the same quantity, delivery term, and packaging basis. A cheaper insert can become expensive when cartons arrive late or mixed sizes need manual sorting. Ask for a realistic lead time and a written process for nonconforming parts. Leave room for uncertainty. Exchange rates and port delays can shift budgets, so test a modest-delay scenario before committing.

Scroll to Top